Octagonal Cage Manufacturer Insights: Choosing the Right Partner for Durable Custom Solutions
2026-09-07
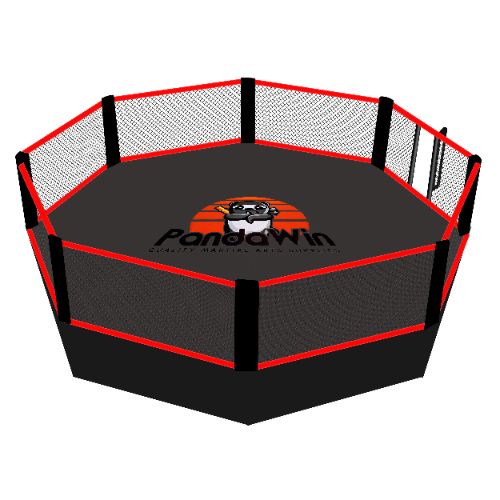
Choosing an octagonal cage manufacturer isn't just about steel thickness—it's about finding a partner who understands the demands of combat sports. At PandaWin Sports, we've seen too many operators settle for cages that wobble under pressure. This guide breaks down what separates durable custom solutions from disposable ones, so you can make a decision that protects your fighters and your brand.
The First Sign of a Reliable Octagonal Cage Builder Isn't on the Quote
Most buyers fixate on the bottom line, but the first clue you're dealing with a builder who actually understands octagonal cages comes earlier, often in the questions they ask before pricing. A solid shop will want to know how the cage will be used, whether it will live indoors or outdoors, the expected weight and movement of what goes inside, and how often panels need to be taken apart. If a builder quotes a flat rate without mentioning corner angles, joint reinforcement, or panel flex, that quote is guessing, not engineering.
The geometry of an octagon punishes sloppy fabrication quickly. Eight corners mean sixteen connection points that must align within tight tolerances, otherwise doors bind, welds stress, and the whole structure pulls out of square. A dependable builder tends to talk about how they fixture the frame, what thickness they recommend for the diagonal bracing, and why certain joints get gussets instead of simple welds. Those details rarely show up on a quote, but they show up the first time the cage gets moved or hit hard.
Why Custom Cage Projects Stumble When Engineering Gets Skipped
Skipping the engineering phase on a custom cage build feels like a shortcut until the first test fit. A design that looks perfectly balanced on a screen can hide clearance issues, weak joints, or mounting points that simply don't line up with the vehicle's actual structure. Without proper load path analysis and material selection, you end up with a cage that adds weight without adding safety, forcing expensive rework or complete scrapping of fabricated sections.
The most common failure point isn't exotic—it's the connection between the cage and the chassis. Hand-drawn sketches or generic templates rarely account for production tolerances, existing wiring harnesses, or how the body flexes under dynamic load. When engineering is skipped, builders often overcompensate with thicker tubing or extra gussets, which only shifts stress to unintended areas. The result is a cage that passes a visual glance but falls short under real-world conditions, creating a false sense of security.
Another overlooked consequence is serviceability. A cage designed without considering seat removal, pedal access, or future modifications turns routine maintenance into a nightmare. Engineering isn't just about crash safety—it's about integrating the cage into the car's life cycle. When that step is missing, the project stalls not because of ambition, but because the foundation was never validated against measurable requirements.
Material Grade Matters More Than Wall Thickness Alone
Focusing only on wall thickness can lead to a false sense of security. A thicker wall made from a lower-grade material often fails earlier under cyclic stress, chemical exposure, or temperature swings than a thinner wall using a high-performance alloy. The internal structure, grain refinement, and impurity controls in a higher material grade directly affect crack resistance and long-term stability.
Real-world failures frequently trace back to grade selection rather than insufficient thickness. For instance, in aggressive environments, a premium corrosion-resistant grade at a moderate wall thickness can outlast a basic carbon steel with twice the wall dimension. This is because material grade determines how the metal behaves at a microstructural level, not just how much metal is present.
Welding Quality You Can't Fake Under Powder Coat
A smooth powder-coated finish might hide a lot of surface sins, but it will never hide what happens underneath a bad weld. Cracks, incomplete fusion, and undercut show up later as stress points once the frame is loaded, flexed, or left outside through a few seasons. The coating simply follows the joint—so if the weld profile is uneven or porous, that texture remains visible and the weak spot is already built in.
That’s why weld inspection has to happen before any coating goes on. Penetration is checked at the root, bead consistency is verified along the full length, and any repair is re-tested rather than filled with paint. A truly structural weld looks clean even before powder coat, and it stays strong long after the color starts to fade.
How Smart Fabricators Handle Non-Standard Dimensions
Standard tolerances rarely survive contact with a real-world blueprint. Smart fabricators know that odd fractions, metric-imperial swaps, or a frame drawn 1.5 mm out of square are not anomalies—they are the daily reality. The first move is always to measure from the actual part, not from memory or a clean CAD file. A plate that looks flat on screen might have a crown, a bend radius that isn’t quite 90 degrees, or a hole pattern drifted by wear on the jig. Rather than forcing the part to match the drawing, the fabricator asks what the drawing was trying to achieve: does this surface need to seal, slide, or carry load? That answer drives the correction, not the nominal dimension.
What separates a good shop from a great one is the habit of building adjustment into the workflow before the first cut. Instead of cutting every piece to the listed size, smart fabricators leave one or two edges deliberately oversized, then fit them in sequence. A corner that measures 89.7 degrees gets welded, clamped, and shimmed until the opposing panel sits flush. Non-standard dimensions also reveal gaps in equipment: a brake press rated for 8 feet won’t fold a 10-foot sill, so the team pre-bends in sections, checks the kink line with a straightedge, and stitches the seam with a backer plate. No one waits for a miracle machine—they adapt a fixture, make a temporary stop, or hand-fit the odd piece.
Finally, smart fabricators document the deviation, but not as an excuse. A small handwritten note on the cut sheet—“flange trimmed 0.8 mm to clear the existing bolt head”—becomes the tribal knowledge that prevents the same fight next week. They also know when to push back: if a customer’s “non-standard” dimension is simply a typo carried over from an old revision, a five-minute phone call saves a day of rework. Handling odd sizes is less about perfect math and more about accepting that the part in your hand is the true drawing. The fabricator’s skill is in reading that physical truth and making the metal agree with it.
What Long-Term Durability Actually Costs—and Where Corners Get Cut
The price tag on a durable product rarely reflects its true long-term cost. A frame that survives a decade of hard use without flexing, cracking, or corroding demands more than just thicker steel—it requires precise alloys, controlled heat treatment, and welds that don't introduce weak points. When you pay less upfront, you're often buying into a cycle of frequent replacements, downtime, and hidden labor expenses that dwarf any initial savings.
Corners get cut in places most buyers never inspect. Cast fittings replace forged ones because they machine faster, even though they snap under shock loads. Powder coating gets thinner or skipped entirely on hidden surfaces, inviting rust from day one. Bushings and bearings shrink in size, concentrating stress until they egg out. Fasteners lose their plating, threads strip, and suddenly a simple repair becomes a full teardown. These aren't accidents—they're deliberate choices made to hit a retail number that looks competitive on a shelf.
The real cost difference shows up after five years. A higher-quality assembly might cost 40% more initially, but it won't need its third set of pivot bolts, a re-welded bracket, or a weekend lost to unplanned maintenance. That's the durability premium: not what you pay at checkout, but what you never pay later. Any manufacturer can build something cheap that survives a season. Building something that stays tight, true, and rust-free after a decade is a different engineering discipline entirely.
FAQ
Look beyond glossy catalogs. Check whether they ask about your actual use case, offer material samples, and can explain how their welding and coating processes affect long-term performance. A good partner will discuss stress points and access requirements instead of just quoting a price.
Not automatically. The eight-sided shape distributes stress more evenly across joints, but strength depends on material gauge, weld quality, and bracing. When designed properly, octagonal cages reduce sharp corners and can handle lateral force more gracefully in high-traffic or animal housing settings.
You can typically specify bar spacing, door placement, panel materials, coating type, and even modular connectors for future expansion. Some manufacturers also offer options like removable trays, perch mounts, or lockable access points if you ask early in the design phase.
Request a sample panel or small prototype. Ask for close-up photos of welds and coating thickness data. Independent material certifications, like mill test reports for steel or aluminum, also help you confirm that what is promised is actually being used.
Powder coating usually wins for outdoor use because it creates a thicker, more uniform layer that resists UV fading and moisture better than standard liquid paint. It also bends slightly with metal expansion, reducing the chance of micro-cracks that lead to rust.
For most custom octagonal cages, expect two to four weeks for a sample or first article, then another four to eight weeks for batch production after approval. Complexity, material availability, and special packaging can push those windows out, so confirm milestones before committing.
Buyers frequently forget to confirm packaging and palletizing standards, edge protection for powder-coated panels, and how doors or removable parts will be wrapped. These oversights cause more damage in transit than manufacturing defects.
Send clear dimensional drawings or sketches, material preferences, target quantity, delivery location, and any relevant usage conditions like weather exposure or animal contact. The more context you provide, the fewer assumptions the manufacturer has to make, and the more precise the quotation will be.
Conclusion
Most buyers fixate on the bottom line, but the first real signal of a dependable octagonal cage builder shows up before any numbers are shared. It's in how they talk about load paths, joint design, and the specific demands of non-standard dimensions. When engineering gets skipped to rush a quote, projects stall later—warped frames, mismatched angles, and field modifications that blow the budget. A shop that asks about your actual use environment, from vibration to weather exposure, is already protecting you from those hidden failures. The right partner treats the quote as a technical document, not a sales pitch.
Material grade matters more than wall thickness alone—a thinner high-strength steel can outperform a thicker mild steel in fatigue. But that advantage disappears if welds are porous or undercut, flaws that powder coat hides until stress reveals them. Smart fabricators don't pretend every dimension fits a standard jig; they adjust fixture points, sequence welds to control distortion, and verify fit before coating. Long-term durability has a real cost, and it's usually not in the raw material price—it's in the extra passes, inspection time, and refusal to cut corners on joints that won't be seen again after finishing. That is why the right partner rarely offers the cheapest quote—they offer the one that won't need rework in year two.
Contact Us
Contact Person: Fei Xu
Email: [email protected]
Tel/WhatsApp: +8618631245578
Website: https://www.pandawinsports.com/