Sanding Disc Factory Insights: What Makes a Reliable Abrasive Supplier
2026-10-08
Ever wondered why some sanding discs wear out after a few passes while others keep cutting clean? The difference often comes down to the factory behind the product. A truly reliable abrasive supplier isn’t just a source of materials—it’s a partner in your finishing quality. In this post, we pull back the curtain on what to look for, from raw grit selection to bonding consistency. And if you’re tired of unpredictable batches, SHENZHEN SUN ABRASIVES is one name that keeps surfacing in these conversations.
Raw Material Lots That Fail Before the First Disc Is Pressed
A batch can look perfect on paper and still get rejected the moment it hits the hopper. We’ve had lots where the melt flow index drifts just enough to change fill behavior in the mold, leaving short shots or flash that no amount of cycle tweaking can fix. Sometimes it’s not the resin itself but what’s hiding in it: metal fines from a supplier’s grinding line, carbonized specks from a poorly purged extruder, or moisture that turns to steam and blows pinholes through the puck.
The harder cases are the ones that pass the standard lab panel but fail under real press conditions. A lot might hold its color until you run it at full barrel temperature, then shift toward amber. Another might carry enough static to clump in the feed throat, starving the screw and throwing shot weight all over the map. These aren’t failures you can fix downstream; they get flagged, quarantined, and sent back before the first stamper ever comes down.
Grit Adhesion Tests Under Real Backing Flex
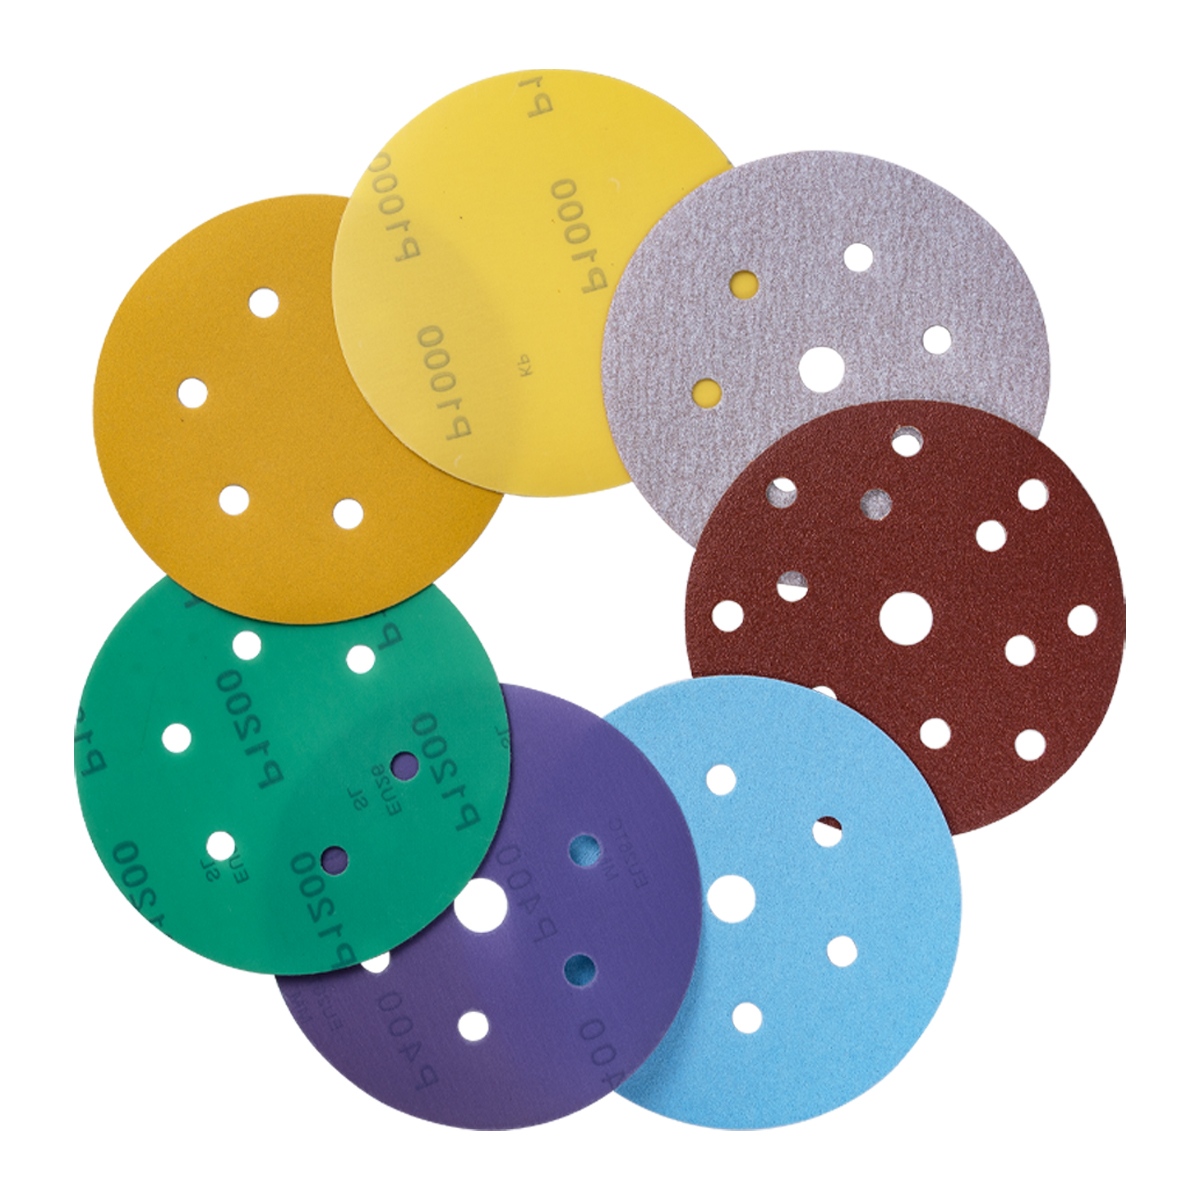
Coated abrasive performance often looks great in a static pull test, yet the real story emerges only when the backing bends, twists, and flexes under actual sanding pressure. That is why grit adhesion tests under real backing flex mimic the working conditions of a belt running over a contact wheel or a disc pressed into a curved surface. Instead of simply measuring how much force it takes to pop a grain off a flat sample, these tests cycle the backing through repeated bending while simultaneously subjecting the abrasive surface to controlled wear. The result reveals weak points that conventional adhesion tests miss, such as grain clusters near the splice or micro-cracks that propagate from stress concentration zones.
A practical setup often uses a flexing rig where a coated abrasive strip runs back and forth over small-diameter rollers at a set tension and speed. A weighted contact block or a counter-rotating drum applies normal load to the grit side, gradually abrading the surface while the backing endures thousands of flex cycles. After each interval, the number of lost grains per unit area is counted, and the failure mode is classified: clean grain pull-out, resin fracture, or backing delamination. This distinction matters because a grain that pops out whole indicates poor wetting or under-cure, while fractured resin around a remaining grain stump points to brittle binder chemistry. Tracking these patterns across flex cycles provides a far more realistic durability profile than a single-point adhesion value.
One of the biggest differentiators in the field is how tests handle simultaneous multi-axis stress. Many abrasive products see not just longitudinal bending but also twist and lateral shear, especially on narrow belts or flap discs. Advanced rigs therefore add a gentle oscillating twist component or an offset roller that forces the backing into a mild S-curve. Under such conditions, otherwise acceptable grit retention can drop sharply, exposing resin systems that are too rigid or backings that fatigue prematurely. By comparing weight loss, grain protrusion, and surface roughness after a fixed number of flex cycles, manufacturers can fine-tune both the make coat and the backing treatment. The outcome is a more honest specification: not just "good adhesion," but adhesion that survives the way the abrasive is actually used in the field.
Resin Cure Profiles That Decide Disc Consistency
Resin cure profiles shape disc consistency long before the first grind. The initial temperature ramp sets the pace for volatiles to escape and for the resin to wet the abrasive grain evenly. If the ramp is too steep, the outer skin cures first and traps moisture or solvent inside, leaving a disc with a hard shell and a soft, under-cured core. That imbalance shows up later as uneven wear, chatter, or premature loading. A gentler, staged ramp lets the whole mass cross the gel point at roughly the same time, which is what gives the disc a uniform working face.
Dwell time at peak temperature often matters more than the peak number itself. A short dwell leaves partially crosslinked regions scattered through the bond, and those weak spots break down faster under load. Over-curing, on the other hand, makes the resin brittle and prone to edge chipping. The real target is thermal equilibrium across the entire disc stack during the hold, not just the oven air temperature. Some shops add a brief intermediate soak or a post-cure annealing step to smooth out temperature gradients that would otherwise hide in the finished disc.
Cooling rate after cure is the quiet variable that decides flatness and residual stress. A fast quench can warp the disc or freeze in microstresses that later release as cracks or thickness variation. Controlled cooling, especially through the glass transition range, lets the resin relax without losing its crosslink structure. Discs cooled this way tend to stay flatter on the flange and deliver more predictable cutting or polishing behavior from batch to batch.
Backing Plate Selection Beyond Thickness and Flexibility
While thickness and flexibility often dominate initial screening, real-world performance hinges on less obvious factors. Thermal conductivity and heat capacity of the backing material directly influence how quickly pad temperatures stabilize, which in turn affects friction consistency during repeated stops. A plate that insulates too well may keep the friction surface hotter than intended, while one that conducts aggressively can transfer excessive heat into the caliper piston and brake fluid.
Surface treatment and edge geometry also deserve attention. Anodized or galvanized layers do more than prevent corrosion; they alter the micro-texture where the pad meets the piston and shims, changing the way vibrations are damped or amplified. Chamfered edges, radial slots, or relief cuts can shift dust evacuation patterns and even alter cooling airflow across the rotor face, making a measurable difference in pad taper wear and noise behavior under hard use.
Finally, match the plate to the specific caliper and hub environment rather than chasing universal upgrades. Some designs integrate tuned mass dampers or viscoelastic coatings that suppress a narrow band of squeal frequencies, but these only work when the surrounding hardware is stiff enough to support them. Checking runout, piston contact area, and abutment clearance often reveals more about long-term satisfaction than a simple bend test or thickness gauge ever will.
Batch Coding as a Mirror of the Production Floor
Walk any line at a mid-size food plant and you'll see it quickly: the batch code stamped on a pouch of sauce, a carton of frozen pastry, a bottle of cleaner. It looks like a throwaway string of digits, but it's actually a snapshot of the shift that made it. The date, the line number, the time window, sometimes the operator's station—all compressed into ink. When a recall hits or a customer complains about off-flavor, that code becomes the first clue, not because it explains the chemistry, but because it pins the moment and place of production.
The same code is also a mirror of how disciplined the floor really is. A line that runs clean, with changeovers logged accurately and equipment cleaned on schedule, produces batch codes that match the paperwork. When codes get smudged, misread, or skipped, it rarely happens in isolation; the same crew might be cutting corners on temperature checks or letting allergens linger. Supervisors who spend time reading codes at the end of a shift often find small irregularities—a missing lot suffix, a timestamp that doesn't match the shift roster—that point to larger gaps in training or staffing.
At its best, batch coding turns the production floor into something legible without a single extra meeting. A well-designed code sequence tells you at a glance whether the line was running at speed, whether a rework batch got mixed in, and whether the sanitation crew had enough time between runs. It won't fix a worn bearing or a mislabeled ingredient, but it will show you where to look. In that sense, the ink isn't just compliance; it's the floor's own handwriting, and learning to read it is cheaper than installing another sensor.
Custom Orders That Don't Start with a Canned Quote
Most quoting workflows begin with a template that gets tweaked here and there until it sort of fits. That approach works for simple, repeatable jobs—but breaks down the moment a project has unusual dimensions, mixed materials, or a deadline that doesn't line up with standard lead times. We skip that step entirely. Instead of pulling a pre-built price sheet off the shelf, we start by asking what you're actually trying to build, where it will live, and what constraints you're working under. The quote grows out of those answers, not the other way around.
The process itself is deliberately low-friction. You send us a sketch, a photo, a napkin drawing, or just a few paragraphs describing the function. We read it carefully and come back with targeted questions—usually about tolerances, finish expectations, or whether the part needs to interface with existing hardware. Only after those details are pinned down do we put numbers to anything. That back-and-forth might take a couple extra days compared to an instant online calculator, but it prevents the kind of surprises that show up later as change orders or rejected prototypes.
What you get at the end is a quote that reflects the actual scope, not a padded estimate built to cover unknowns. We itemize materials, labor, and any outside processes like plating or heat treating, so there's no vague "miscellaneous" line hiding a markup. If the budget doesn't fit, we'll tell you which specs are driving cost and suggest alternatives—a different alloy, a simpler geometry, a batch size adjustment. That collaborative approach means the final number is something you can take to your own stakeholders without having to defend guesswork.
FAQ
Pay attention to how the factory handles raw material storage and mixing. Consistent grit distribution and uniform resin application on the backing material usually indicate stronger quality control than a spotless showroom.
The backing weight, bond type, and grain quality all affect lifespan. A disc made with cheaper heat-treated aluminum oxide may shed grains quickly, while a well-bonded ceramic blend holds up longer under pressure.
Ask how they adjust formulations for different materials like stainless steel versus softwood. A supplier who asks about your sanding pressure, machine speed, and finish requirements is more likely to provide the right product than one who ships a generic catalog item.
Many do, but the lead time and minimum order quantity can vary a lot. Some factories keep stock of standard film, paper, and cloth backings and can punch custom hole patterns quickly, while others treat every non-standard request as a new production run.
Look for batch-level test results covering grain adhesion, dimensional tolerance, and burst speed, not just a general ISO certificate. Honest suppliers will share photos or videos from their own testing lab when you ask about a defect.
Often the discount comes from using recycled backing material, thinner adhesive layers, or wider tolerance on grit size. These discs can still work for rough sanding but tend to leave inconsistent scratches and produce more dust.
Poor dust extraction during coating can cause grit contamination between different abrasive grades. A well-designed factory separates production areas and uses anti-static treatments so fine particles don't stick to the open coat.
Quick response on technical complaints and a willingness to adjust the next batch beats a long warranty document. The best suppliers treat problems as an opportunity to learn your specific sanding conditions.
Conclusion
A dependable sanding disc factory reveals its character long before a finished product reaches the shelf. Raw material batches that fail initial checks are pulled aside before the first disc is even pressed, preventing weak lots from ever entering the production stream. That early discipline sets the stage for what follows. Grit adhesion is not judged on static panels alone; it is tested under real backing flex, mimicking the bending and tugging a disc endures in actual use. When the backing flexes, poorly bonded abrasive falls away quickly, so only formulations that hold up through repeated flex cycles move forward. Resin cure profiles then decide whether every disc behaves the same way. A reliable supplier monitors time and temperature curves closely, because small deviations in curing can leave some discs brittle and others too soft, even from the same batch.
Beyond the obvious specs, backing plate selection goes far deeper than thickness and flexibility. The right plate balances heat dissipation, tear resistance, and how the disc seats against a sander's pad, all of which affect comfort and edge wear. Batch coding serves as an honest mirror of the production floor: a clear, traceable code means the factory can pinpoint exactly which resin lot, backing roll, or shift produced a given run. That level of traceability is rare and valuable. Finally, custom orders should never begin with a canned quote. A supplier that asks about your substrate, pressure, speed, and finish expectations before quoting is one that understands sanding as a system, not just a commodity. Together, these details separate a true abrasive partner from a simple disc seller.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn