Servo Motor Magnets Factory: Precision Manufacturing for High-Performance Motors
2026-09-07
When a servo motor needs to deliver split-second precision, the magnets inside are often the unsung heroes. At DAWA, our servo motor magnets factory doesn’t just manufacture components—we engineer the magnetic core that defines torque, speed, and reliability. Curious how we achieve tolerances down to the micron while scaling for high-volume production? Read on to discover the craftsmanship behind every high-performance motor.
Where Rotor Magnets Earn Their Specs
The specification sheet is where rotor magnets stop being abstract components and start being accountable. Every value printed there is a promise the magnet has to keep once it's spinning at speed inside a motor. Torque curves, temperature tolerance, and flux density get pinned down on paper long before the first prototype ever hits a test bench.
A solid spec doesn't just list numbers; it explains the trade-offs. A rotor magnet that delivers high remanence might sacrifice coercivity, meaning it holds a strong field but demagnetizes under heat or opposing currents. Engineers read between those lines to see how a magnet will actually behave when the motor is pushed past its comfort zone.
That's where rotor magnets truly earn their keep: in the details that survive the transition from datasheet to dynamometer. Peak efficiency, back-EMF constants, and mechanical tolerances aren't just marketing bullet points. They are the difference between a motor that launches smoothly and one that throws a rotor out of balance at 12,000 rpm.
The Tolerance Game That Separates Good from Great
Most people mistake tolerance for passive suffering—putting up with more pain, waiting longer, or smiling through frustration. That version only gets you to "good." The great ones treat tolerance as a sorting mechanism: they lean into discomfort that sharpens their judgment and quietly exit situations where the pain has stopped teaching them anything.
The difference becomes obvious when plans fall apart. A good performer can absorb a bad quarter, a hostile client, or a delayed launch without breaking. A great performer does something stranger—they stay curious about exactly which part of the failure is tolerable and which part signals a deeper mismatch. That distinction prevents them from grinding through the wrong hardship.
In practice, this looks like patience with unresolved tension. Instead of rushing to fix a messy negotiation, a weak signal in the data, or a teammate's half-formed idea, they let the ambiguity sit long enough to reveal its shape. The tolerance isn't passive; it's an active willingness to live in the gap between what they expected and what is actually emerging. That gap is where good stops and great begins.
From Raw Alloy to a Motor-Ready Magnetic Arc
You start with a batch of rare earth metals and iron, melted under a controlled atmosphere until the mixture reaches a precise chemical balance. The molten alloy is then rapidly quenched into thin flakes, locking in a fine-grained microstructure that will later define the magnet's coercivity. These flakes are milled into a fine powder, aligned in a magnetic field, and compacted under immense pressure to form a dense green body. Only then does sintering fuse the particles together, followed by precise machining to achieve the tight tolerances a motor demands.
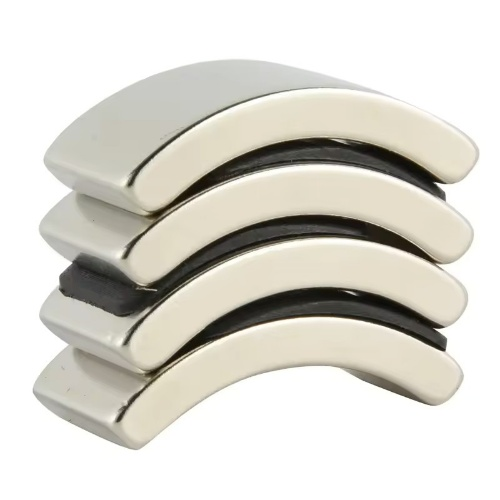
Once the blank emerges from the furnace, it is far from finished. Diamond grinding shapes the arc segments to fit the rotor curvature exactly, while chamfers and edge breaks prevent stress concentrations during assembly. A multi-stage coating process—often nickel, copper, and a top layer of epoxy or parylene—shields the reactive neodymium-iron-boron core from corrosion. Each segment then undergoes full magnetization in a dedicated fixture, imprinting the desired pole pattern. The result is a magnetic arc that delivers high flux density with minimal eddy current losses.
Quality checks at every stage separate a motor-ready arc from a near miss. Automated vision systems measure dimensional accuracy to within a few microns, while flux mapping verifies the magnetic field profile across the entire arc surface. Pull tests confirm coating adhesion, and salt spray chambers simulate years of harsh service. Only arcs that pass these gates are packed in magnetically shielded trays, ready to be press-fitted or bonded into rotor assemblies without further adjustment.
Choosing Magnetic Grades Without the Guesswork
Most selection mistakes happen because people start with the highest energy product they can find and then work backward from there. That path leads to expensive magnets, brittle parts, and coating failures you only notice later. Instead, pin down the actual operating point first: what flux density does your air gap need at the maximum expected temperature, and how much demagnetizing field will the magnet see from its own geometry or nearby currents? Once you have those two numbers, grade selection becomes a straightforward lookup rather than a round of samples.
Temperature is where guesswork usually creeps in. A grade that performs beautifully at room temperature can lose a third of its flux at 120 °C, and if you pick a grade with barely enough intrinsic coercivity, that loss becomes permanent. Check the demagnetization curve at the hottest point in the application, not the average operating temperature, and leave at least a 20 percent margin on Hci if the magnet will face any reversed field. This single step eliminates most of the 'it worked in testing but died in the field' failures.
Finally, resist the urge to duplicate a competitor's spec sheet. Their grade choice was likely driven by a supply chain decision, a legacy tooling constraint, or an over-engineered safety factor that no longer applies. Request the full B-H curve from your supplier for the grades you're comparing, plot your load line on it, and verify the minimum energy product you actually need. Often you'll find a lower-cost grade with the same usable flux, because the difference between N35 and N52 rarely matters once the magnet is inside a closed magnetic circuit.
Heat Soak and Demag Curves: The Unforgiving Tests
Heat soak testing pushes magnets to their thermal limits and watches for the moment performance starts to slip. A sample is held at elevated temperature for extended periods, then measured against its original demagnetization curve. Even a few percent loss in flux density can mean the difference between a reliable motor and a field failure, so engineers treat these numbers as hard pass/fail gates rather than rough guidelines.
The demag curve itself is brutally honest. It shows exactly where a magnet’s working point collapses under opposing fields at temperature. When a design sits too close to the knee of that curve, heat soak data becomes the tiebreaker: either the material survives the worst-case thermal soak without irreversible loss, or the whole design goes back to the drawing board. No amount of simulation confidence replaces that measured curve after the oven door finally opens.
Custom Geometries That Drop Into Existing Rotors
One of the biggest headaches in rotary equipment upgrades is finding a geometry that actually fits the housing you already own. Custom geometries solve this by matching the exact bore, width, and seal groove dimensions of your current rotor profile. No adapter plates, no re-machining the casing, no shimming tricks that only last a few hundred hours. The new lobes or screws slide straight in, using the same bearings and timing gears, which keeps downtime to a single shift instead of a full teardown.
The real advantage shows up when you need to change performance without changing the rotor diameter. For example, a three-lobe helical geometry can replace a straight two-lobe set and cut pulsation by half while boosting volumetric efficiency at low speeds. Because the profile is generated from your existing rotor center distance and housing clearance, the thermal growth and deflection behavior stay predictable. You get the flow curve you need, not an approximation that forces you to re-rate the entire blower package.
Installation is deliberately boring: drain the oil, pull the old rotors, inspect the bearings, drop in the new geometry, and set the timing marks. No laser alignment of the casing, no welding on new flanges. That means the same spare gear set and seal kit stay on the shelf, and your maintenance crew doesn't need to learn a new machine. It's a retrofit, not a replacement, and that's the whole point.
FAQ
They create the rotor field that interacts with the stator windings. Any deviation in flux density or magnet shape directly shows up as torque ripple or positioning error, so precision in these parts is a prerequisite for smooth control loops.
After sintering, each magnet goes through profile grinding and wire EDM where needed. We measure critical faces with a coordinate measuring machine and sort by thickness within a few microns before magnetization.
Most designs use high-coercivity neodymium grades such as N42SH or N48H, depending on operating temperature. For higher-temperature servos we may recommend N35EH or samarium cobalt if demagnetization risk is a concern.
Yes. We regularly produce skewed arcs, radial rings, and multi-pole ring magnets with anisotropic orientation. The tooling and pressing process are adjusted for each geometry to keep the easy axis aligned with the intended field pattern.
Standard options include nickel-copper-nickel, epoxy, and parylene coatings. For motors exposed to coolants or humidity, we often suggest a nickel plus epoxy topcoat after salt-spray testing to verify adhesion and coverage.
We track magnetic properties, coating thickness, and mechanical dimensions for every production lot. A sample from each batch is magnetized and tested for flux density, and the full data set ships with the parts so the motor builder can adjust rotor assembly if needed.
Conclusion
Inside a servo motor magnets factory, the work is less about simply casting magnets and more about engineering every rotor arc to earn its place under load. The process starts long before any magnet is pressed—raw alloy selection determines the magnetic grade, whether that's a cost-conscious neodymium variant or a high-coercivity grade built to survive aggressive demagnetization. From there, the blend is milled, aligned, and compacted into arcs that must hit dimensional windows measured in microns, because even a slight deviation in arc radius or thickness changes how the rotor cogging feels. That tolerance discipline separates a smooth, quiet motor from one that vibrates under speed. But geometry is only half the story. Heat soak tests and demag curve tracing push finished magnets through temperature cycles and opposing fields, verifying they won't lose flux when the servo runs hot and hard.
What really sets a strong factory apart is how it handles the variables customers bring to the table. Instead of forcing buyers to guess at magnetic grades, the engineering team works backward from peak torque, top speed, and ambient temperature. That kind of grade selection without guesswork means fewer over-specified magnets that waste cost or under-specified ones that fail in the field. And because many retrofits and new builds already have existing rotor lamination stacks, custom geometries—odd pole counts, skewed arcs, or segmented magnets—are matched to drop straight into those slots without redesigning the rotor. The result is a magnet that doesn't just meet a datasheet; it behaves predictably inside the actual servo motor, from first spin to thousands of hours under thermal and electrical stress.
Contact Us
Contact Person: Kelvin Lo
Email: [email protected]
Tel/WhatsApp: 0769-88561131
Website: https://dawamagnetic.com/